ANSI/ASQ Z1.4 AQL Calculator — Sample Size, Accept & Reject
Major Defects
Minor Defects
AQL Sampling Guide
ANSI/ASQ Z1.4 (ISO 2859-1) inspection sampling guide & Product Category Applications
17+ Years Experience
Serving global buyers since 2009 with 5,000+ product inspections in China across 50+ countries
Inspection Cost Estimator
Estimate Inspection Cost by inputting product category, quantity, AQL sampling size
Embed This Tool
Copy the code below to embed this ANSI/ASQ Z1.4 AQL calculator directly on your website or blog.
Special Inspection Levels (S-1 to S-4): When Testing Puts the Sample at Risk
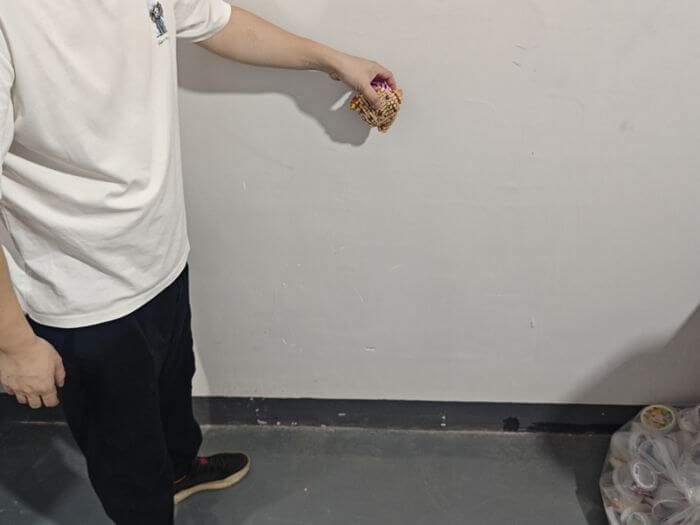
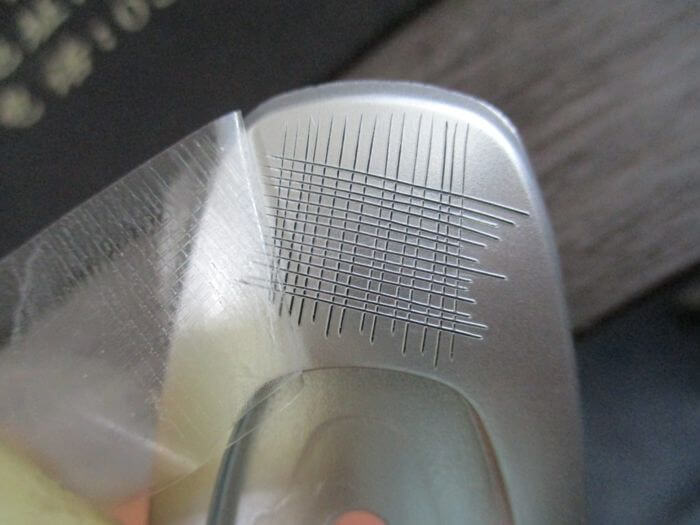
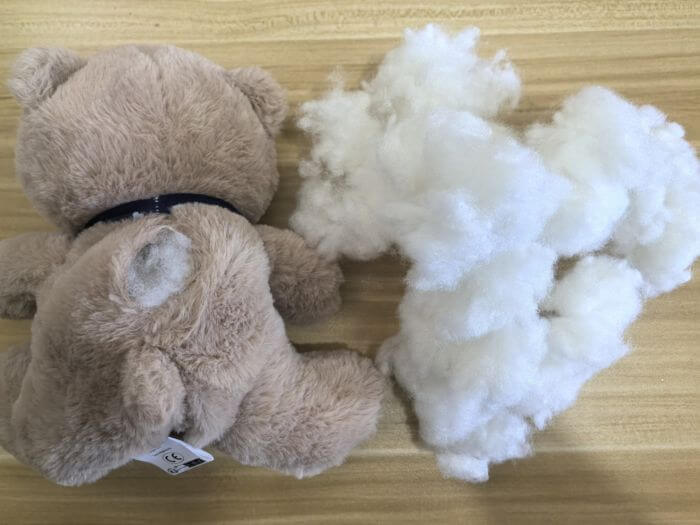
General Inspection Levels answer "is this lot acceptable?" Special Inspection Levels answer a different question: "how many units can we afford to put at risk to find out?" The tests that drive a special level carry a risk of product damage — not certain destruction. Some do consume the sample outright (a cross-cut grid cannot be un-cut); others only put it at risk: a structurally sound unit may pass a drop test or a hi-pot test unharmed, but you cannot know in advance which units will survive, and tested units do not return to stock as first quality. The most common examples: drop tests, hi-pot tests, coating adhesion, moisture readings and inner-cleanliness checks. A 5,000-piece lot cannot spare 200 units for carton drops. The standard's answer is a set of deliberately tiny sample sizes, S-1 through S-4, reserved for special, functional and damage-risk tests.
These are the tests that, in 17 years of on-site independent quality control inspection, most often force a special level.
Damage-risk and destructive tests
Equipment-dependent special checks
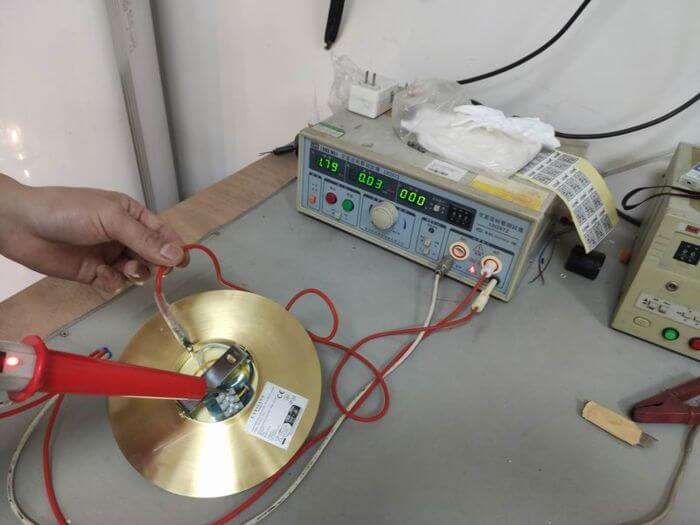
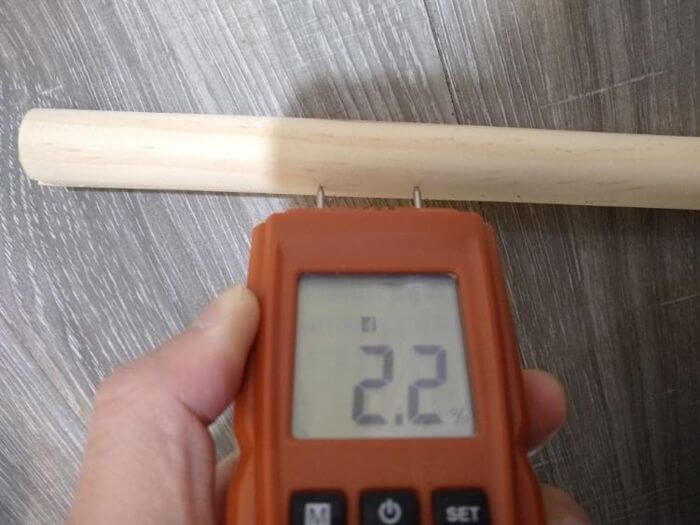
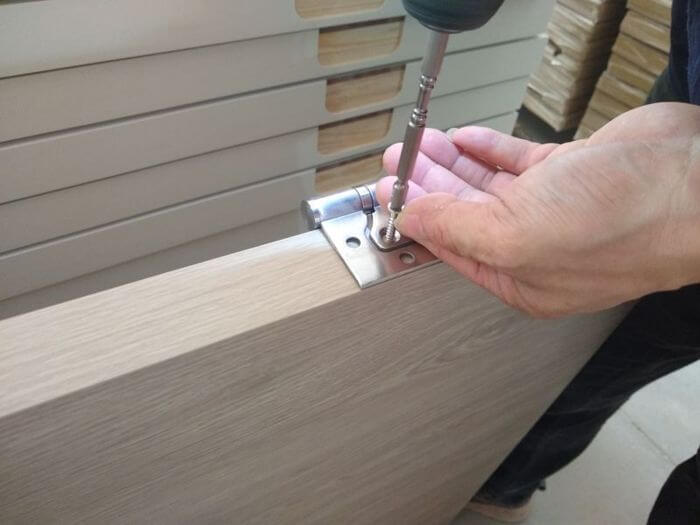
Field practice vs. the standard table: this calculator strictly follows the ANSI/ASQ Z1.4 (ISO 2859-1) master tables, including arrow-tracking rules that may automatically increase sample size to ensure statistical validity. In actual quality control practice, to avoid excessive sample damage and high testing costs, the industry typically uses the base sample size for the given Code Letter (e.g., 8 units for Code D under S-2) and applies a Zero-Defect criterion (Ac = 0, Re = 1), rather than expanding the sample size via arrow tracking. One failed unit rejects the test — and because a failure in these special tests usually points to a design or process problem rather than random variation, zero acceptance is the defensible choice.
What is AQL?
Acceptable Quality Limit (AQL) is the core metric of the ANSI/ASQ Z1.4 and ISO 2859-1 acceptance sampling systems, which are widely used by third-party inspection companies in China. It represents the worst tolerable process average that will still allow a lot to be accepted. For example, AQL 2.5 means that when a supplier's actual defect rate is 2.5% or lower, the sampling plan will accept the lot with high probability.
Normal vs Tightened/Reduced
This calculator uses single normal inspection. Switch to tightened inspection when lot quality is unstable (stricter Ac/Re) or reduced inspection when quality is consistently good (smaller sample size).
Major vs Minor Defects
Major defects affect function, safety or regulatory compliance; Minor defects are cosmetic or usability issues that do not affect function. Major AQL is usually lower than Minor AQL.
Why On-Site Quality Control Inspection Matters
AQL tells you how many to inspect and how to decide, but random sampling, testing methods and defect classification still require a trained inspector on site.
How to Use This ANSI/ASQ Z1.4 AQL Calculator
- Select the Lot Size range closest to your order quantity.
- Choose the Inspection Level; General II is the default for most consumer goods.
- Set the Major AQL and Minor AQL separately; Major is usually stricter.
- Click Calculate to see sample size, Ac, Re and a plain-language explanation.
Tip: Share a specific result via URL parameters, e.g. ?lot=1201-3200&level=II&major=2.5&minor=4.0.
Prefer to read the values straight off the standard tables — or to see several AQL columns side by side — use our AQL chart and sampling tables. It also covers what the arrows mean, when a lot has to be split, and why a reworked lot cannot simply re-enter the same plan.
What Counts as a Lot (Batch) in AQL Sampling
A lot (batch) is a quantity of the same product made under the same conditions and offered for product inspection at one time. Fill the Lot Size field with the total number of units in that lot — not with the sample you expect to check, and not with the number of cartons.
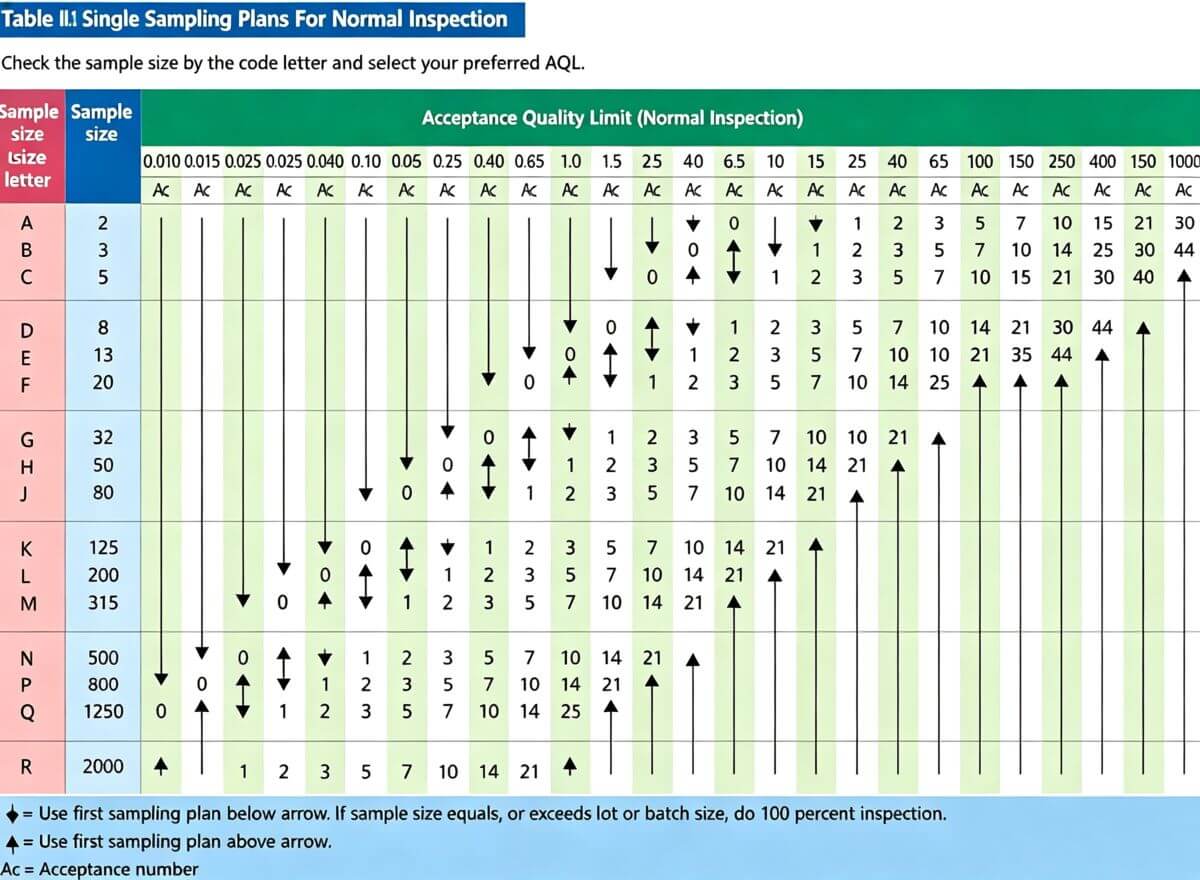
Select the band your total quantity falls into: 2–8, 9–15, 16–25, 26–50, 51–90, 91–150, 151–280, 281–500, 501–1,200, 1,201–3,200, 3,201–10,000, 10,001–35,000, 35,001–150,000, 150,001–500,000 and 500,001+. These are the lot-size bands of ANSI/ASQ Z1.4 and ISO 2859-1, and the band you land in sets the sample size code letter, which in turn fixes the sample size and the accept and reject numbers.
Two situations are worth checking before you run the numbers:
- An order split into several shipments. An accept or reject decision is made per lot, so if one order is produced or shipped in separate runs on different dates, run the calculator once for each lot instead of once for the whole order.
- Very small lots. When the standard sample size is larger than the lot itself, the tool switches to full inspection and tells you below the result.
Critical, Major and Minor Defects: What Each Class Means for Your Lot
Defect classification is what turns a sample into a decision. Below are the three classes widely used by third-party product inspection for consumer goods:
| Defect class | Definition | Typical examples | Effect on the lot |
|---|---|---|---|
| Critical | A safety hazard, a regulatory violation, or a defect that makes the product unusable as intended | Live voltage on an accessible metal part; a banned substance in a toy; a blade that breaks inside the housing | No AQL is applied. One unit found is enough to reject the lot, and 100% quality inspection is required before shipping. |
| Major | A defect that affects function, safety in use, or the ability to sell the product as intended | A zipper that jams; a switch that works only intermittently; a missing component in the box | Judged against the Major AQL — commonly 2.5 — through the accept and reject numbers. |
| Minor | A cosmetic or finish deviation that leaves function and compliance intact | A slight colour shift; a light scuff on a hidden surface; uneven stitching along a seam | Judged against the Minor AQL — commonly 4.0 — through the accept and reject numbers. |
The same physical flaw can change class depending on where it appears: a scratch on a display lens is major, while the same scratch on the base is usually minor. Classification also has to be agreed before inspection service starts, otherwise the accept and reject numbers mean nothing. In practice it is applied on site by the inspector, which is why buyers pair the sampling table with independent inspection services in China instead of sending the table to the factory on its own.
Why AQL Sampling Beats Piece-by-Piece Product Inspection in Quality Control
Checking a representative sample — rather than every single unit — delivers clear advantages for most quality control processes:
- Saves Time & Costs: Significantly reduces inspection overhead without compromising quality standards. Faster inspections mean direct cost savings—especially when working with third-party inspection companies that charge on a man-day basis.
- Balances Risk & Effort: Strikes the optimal balance between catching defective products and maintaining operational efficiency.
- Flexible Standards: Allows tailored AQL levels based on defect severity and product categories.
- Objective Decisions: Provides clear, standardized criteria for batch acceptance or rejection.
You now know the reasoning behind AQL sampling — but might still wonder:
1. Which inspection level best fits your products? Most clients follow the general criteria laid out in our ANSI/ASQ Z1.4 guide.
2. What is a pre-shipment inspection and how does it work to catch defects in your imports? Check the standard procedures we follow for our clients.
ANSI/ASQ Z1.4-2003 (R2018) and ISO 2859-1: Same Roots, Two Standards
"Sample per ANSI Z1.4" is written on thousands of purchase orders every year — by buyers who could not tell you where the standard comes from. The story starts at Bell Labs in the 1920s, where Harold Dodge and Harry Romig built the first statistically grounded sampling tables. During World War II, the U.S. military needed to accept or reject ammunition lots without test-firing every round, and that pressure produced the MIL-STD-105 series. MIL-STD-105E, the 1989 edition, was withdrawn by the Department of Defense in 1995 — which explicitly recommended ANSI/ASQ Z1.4 as the commercial successor. Z1.4 has been revised four times (1971, 1981, 1993, 2003), and the 2003 edition was reaffirmed in 2018. ISO 2859-1 is the international counterpart, last revised in 1999 — and in January 2026 ISO published a third edition that adds skip-lot inspection procedures and incorporates the 2011 amendment.
| ANSI/ASQ Z1.4 | ISO 2859-1 | |
|---|---|---|
| Origin | U.S. commercial successor to MIL-STD-105E, recommended by the DoD since 1995 | International ISO counterpart with the same MIL-STD-105E heritage |
| Current edition | Z1.4-2003 (R2018) | ISO 2859-1:2026 (third edition, January 2026) |
| Main tables | Substantively aligned — same code letters and sample sizes for common consumer-goods plans; differences live in procedural clauses | |
| Typical users | U.S. importers, North American retail programs | EU and Japanese buyers, international programs |
| Latest change | 2003 edition reaffirmed in 2018 | 2026 technical revision adds skip-lot procedures, incorporates Amd 1:2011 |
For consumer-goods inspections in China, both standards produce the same code letters and sample sizes in nearly all common cases — the differences live in procedural clauses, not in the tables your inspector uses on the factory floor. One point worth knowing before your next supplier negotiation: there is no such thing as an "ANSI Z1.4 certification". Z1.4 is a sampling method, not a certifiable management system — the Ac/Re determination belongs in your inspection report, not on a certificate.
Normal, Tightened, Reduced: How AQL Switching Rules Actually Work
Every pre-shipment inspection report we issue states "single sampling, normal severity, General Level II". Almost no buyer asks what "normal severity" implies — yet it is the door to the most overlooked part of Z1.4. The standard is not a stack of lookup tables; it is a sampling scheme designed for a stream of lots from the same supplier, with inspection severity that moves as quality history accumulates:
| Switch | Trigger | What changes |
|---|---|---|
| Normal → Tightened | 2 of 5 consecutive lots rejected on original inspection | Same sample size, stricter Ac/Re numbers |
| Tightened → Normal | 5 consecutive lots accepted on original inspection | Return to baseline acceptance numbers |
| Normal → Reduced | 10 consecutive lots accepted, production stable, and the responsible buyer approves | Smaller sample size (about 40% of normal), higher consumer risk |
| Reduced → Normal | Any lot rejected, or production becomes irregular, or other qualifying conditions fail | Back to baseline sample size |
| Discontinuation | 5 consecutive lots rejected under tightened inspection | Stop inspection under the standard until supplier corrective action is verified |
So why does your one-off pre-shipment inspection always run Normal? Because switching rules need a lot stream. A single PSI is one lot with no quality history behind it — there is nothing to switch. Reduced inspection in particular is a buyer's decision: it cuts cost and sample size in exchange for a higher chance of accepting a deteriorated lot, and most buyers of Chinese consumer goods deliberately never use it. The switching discipline belongs to your ongoing supplier-quality program, not to any individual inspection — which is exactly why a buyer who tracks acceptance history across lots gets more out of Z1.4 than a one-time spot check ever can.
Producer's Risk, Consumer's Risk and the OC Curve: What a Passing Lot Really Means
AQL is the most misread number in quality control. It is not a defect-rate guarantee for a single lot — it is the worst process average that the sampling plan is designed to accept routinely. Every sampling plan balances two errors: producer's risk (α), the chance of rejecting a lot whose quality is actually at or better than the AQL, and consumer's risk (β), the chance of accepting a lot that is genuinely bad. The behavior of a plan is described by its operating characteristic (OC) curve: plot the lot's true defect rate against the probability of acceptance, and you get an S-shaped curve instead of the ideal vertical step.
Below are real binomial numbers for the plan most consumer-goods buyers land on — lot of 1,201–3,200, General II, AQL 2.5: code letter K, sample 125, Ac 7 / Re 8 — compared with a zero-acceptance plan (n=8, Ac=0) as used for damage-risk tests under special inspection levels:
| True lot defect rate | Pa — n=125, Ac 7 (Code K, AQL 2.5) | Pa — n=8, Ac 0 (special level) |
|---|---|---|
| 1.0% | 100% | 92% |
| 2.5% (= AQL) | 99% | 82% |
| 4.0% | 87% | 72% |
| 5.0% | 71% | 66% |
| 6.0% | 52% | 61% |
| 8.0% | 21% | 51% |
| 10.0% | 6% | 43% |
| 20.0% | ~0% | 17% |
Read the left column honestly, because your customers will experience it: a lot running exactly at AQL 2.5 passes essentially every time, and a lot at double the AQL (5% defective) still passes seven times out of ten. Rejection only becomes likely around 6% — two and a half times your AQL. This is the statistical answer to the most painful question in this industry: "the inspection passed, so why did my customers find defects?" Sampling never certifies the units it did not open. It is a risk dial, not a guarantee — and when the dial is not enough, the answer is not a different AQL number, it is 100% full inspection, unit by unit.
The right column explains a subtlety from the special-level discussion above: a zero-acceptance plan sounds absolute — one failure rejects the test — yet statistically it is softer than it sounds, still accepting a 10%-defective lot 43% of the time. Small zero-acceptance samples are cheap alarms for gross failures, not instruments for measuring marginal quality. Knowing which tool answers which question is what separates an inspector who applies tables from one who understands them.
AOQL: The Quality Limit That Applies After a Failed Lot Is Sorted
The OC curve above tells you how a sampling plan decides. It does not tell you what actually ships — because what happens after a rejection matters more than the rejection itself. When a failed lot is screened 100% and every nonconforming unit is replaced or repaired before shipment, the plan stops behaving like a sampling plan and starts behaving like rectifying inspection. The measure that then governs your outgoing goods is the Average Outgoing Quality Limit (AOQL): the worst long-run average percent defective that can leave the process, taken across every possible incoming quality level.
Two things follow from this that most buyers are never told. First, AOQL sits above the AQL. An inspection run at AQL 2.5 does not mean your shipment leaves at 2.5% defective or better; it means the plan was built around a 2.5% process average, which is a different statement entirely. Second, AOQL only exists if the sorting actually happens. If a rejected lot is re-submitted without 100% screening, there is no rectification and no AOQL protection — outgoing quality drifts back toward incoming quality, and the defect rate your customers see is whatever the factory produced.
This is why the wording in your order matters more than the AQL number. “AQL 2.5, General Level II” specifies how the lot is judged. “Failed lots to be 100% sorted and reworked, then re-inspected” specifies what actually protects you — and it is the second sentence that brings AOQL into play. Where sorting is carried out under independent supervision rather than left to the factory, see 100% full inspection. Note too that sorting quality is only as good as the people performing it: the same inspector-judgement problem that governs the original inspection governs the rework, which is why re-inspection after sorting is not a formality.
Frequently Asked Questions
AQL (Acceptable Quality Limit) is the shared language of sampling inspection. It doesn’t guarantee zero defects; it defines the maximum acceptable defect rate per batch, based on ISO 2859-1 / ANSI/ASQ Z1.4 acceptance sampling tables.
Most consumer goods default to General Inspection Level II. Level I samples less (cheaper, riskier); Level III samples more, which suits high-value, high-risk or historically poor suppliers. When unsure, pick II. Want to learn more? Read our complete ANSI/ASQ Z1.4 (ISO 2859-1) AQL Sampling Inspection Guide
2.5 for major defects and 4.0 for minor defects is the most common combination for consumer electronics and toys. Critical defects are never allowed. If the buyer specifies values, follow the buyer.
Randomly draw the sample from the batch: if the defects found are no more than the accept number, the lot passes; if they reach the reject number, the lot fails. In single sampling the rejection number is always one more than the acceptance number (Re = Ac + 1), so the decision is unambiguous. Double sampling instead adds a second, larger sample for borderline results — this calculator follows single sampling, the most common choice for consumer goods.
Three common reasons: the supplier used Level I instead of II, a different AQL value, or double sampling instead of single. Send them this result to align the basis.
Lot size and inspection level fix the code letter, but each AQL is read from the master table separately — when a cell falls in an arrow region, the plan switches to a different sample size (for example Major 500 units at code N while Minor follows the arrow down to 315 at code M). Per ANSI/ASQ Z1.4 clause 9.4 (equivalently ISO 2859-1 clause 10.3), draw the largest required sample and judge each class against its own accept/reject numbers. Our inspectors check all sampled units for both classes — the full 500 — which keeps the plan slightly stricter for the buyer than the table-minimum 315.
Yes. The copy button generates a plain-text summary — lot size, inspection level, AQL values, sample size and accept/reject numbers — that you can paste into an email, a purchase order or a QC report. The result URL (?lot=...&level=...&major=...&minor=...) reopens the same plan for anyone you send it to.
Yes, free. The Embed This Tool section provides an iframe snippet you can paste into your website or quoting system — no registration needed.
It follows the sampling tables of ANSI/ASQ Z1.4 and ISO 2859-1 at Special Inspection Levels S-1 to S-4 and General Inspection Levels I, II and III, with AQL steps from 0.10 to 10.
Critical defects (safety, regulatory or total function failure) are not negotiated within an AQL framework — one found means the whole lot fails and a 100% quality inspection is required. The calculator shows this warning below the result.
Really. No registration and no limits — a common benchmark so buyers, QA and QC teams can align sampling plans in one message.
Both are attribute acceptance-sampling standards descended from the same U.S. military standard, MIL-STD-105E. ANSI/ASQ Z1.4-2003 (R2018) is the de-facto baseline for third-party pre-shipment inspection in China and is typically specified by U.S. buyers; ISO 2859-1 is the international counterpart (third edition published January 2026), more commonly cited by EU and Japanese buyers. For common consumer-goods plans the tables produce the same sample sizes and accept/reject numbers. Note that "ANSI Z1.4 certification" does not exist — it is a sampling method, not a certification.
No — it implements single normal sampling, which is what virtually all one-off pre-shipment inspections use. Tightened and reduced severity belong to Z1.4's switching rules, which apply to a stream of lots from the same supplier over time (for example: 2 of 5 consecutive lots rejected switches you to tightened inspection). A single inspection has no lot history, so it always starts at normal severity.
Yes. AQL is the worst tolerable process average, not a per-lot guarantee. The operating characteristic curve of the common plan (n=125, Ac 7) accepts a lot at exactly 2.5% defective about 99% of the time — and still accepts a lot at 5% defective about 71% of the time. Sampling manages risk; it never certifies the unsampled units. When zero escape risk is required, use 100% full inspection instead.
AQL Calculates the Limit. Our Inspectors Enforce It.
AQL gives the numbers, CNQ controls the quality on the ground. Expert pre-shipment inspections & factory audits across China & Asia.
Contact Your Experts